A mill's busiest day can still be a disappointing trading day. A high volume of paddy may pass through the line while the saleable mix falls short of what buyers ordered. For the Senegal Maktoum–Sarveshwar processing programme, the useful question is how much accepted product the line produces, in each grade, from representative local supplies.
Separate recovery from premium recovery
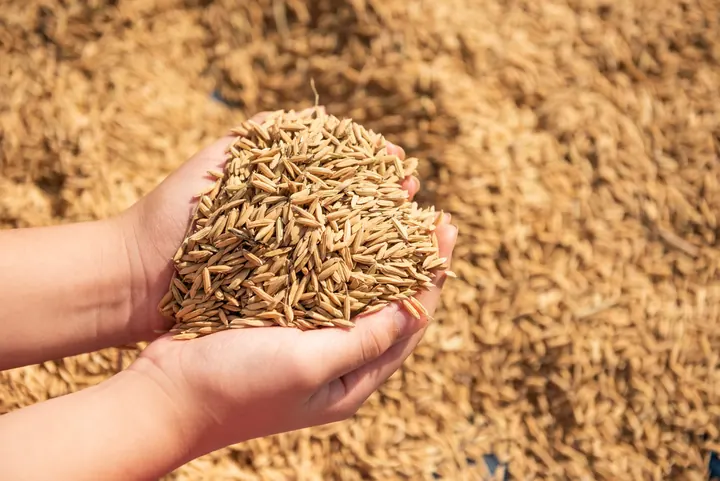
Total milled output and whole-grain output answer different questions. A processing model should distinguish white rice recovery from the proportion sold in the grade a customer values. Broken rice can have a legitimate market, yet its commercial contribution must use its own price, handling and payment assumptions. Counting every tonne at the premium grade price conceals the most important sensitivity. The project team should build a mass balance that follows the input into each product, by-product and recorded loss.
Quality starts before the machinery
IRRI explains that moisture conditions can affect grain breakage and head-rice recovery. The editorial implication is to treat intake quality as part of the mill design. Representative supply lots should be tested before accepting a vendor's performance case. Samples need a known origin, moisture record and handling history, so a favourable result can be connected to an achievable purchasing standard. An exceptional sample chosen for demonstration has little value if the normal procurement programme cannot deliver comparable material throughout the season.
Commission against an agreed product basket
Performance acceptance should cover a sustained run with defined input quality, rather than a brief demonstration of maximum speed. Buyers, operators and the equipment supplier should agree how samples are taken, how output grades are measured and which interruptions belong in the test. The contract can then connect throughput, recovery, consumables and product quality in one record. Where performance changes with variety or moisture, those conditions should be explicit. Otherwise, a seemingly precise capacity promise becomes difficult to interpret when commercial production begins.
Operators should be present during acceptance, because they will inherit the settings and procedures established in the trial. The final handover needs usable instructions, calibration records and a way to identify when normal material falls outside the conditions against which performance was demonstrated. Those records make the test operationally useful.
Give the sales team a usable dashboard
Managers should be able to see the margin generated by a batch after procurement, energy, packaging, losses and rework. A useful report pairs tonnes processed with accepted tonnes by grade and invoices collected. It should also show where quality was downgraded and whether the cause arose at intake, storage or processing. For Senegal, these operating disciplines connect the plant specification with acceptance testing and production reporting. They would help the team decide whether to change suppliers, machine settings or customer commitments before simply increasing the number of operating hours.